+86 18366183241
In the rapidly evolving landscape of global manufacturing, the efficiency, reliability, and precision of pneumatic systems are paramount. Air compressor parts for textile and chemical production represent the beating heart of these industries. The contemporary industrial status reveals a massive shift towards automation, energy conservation, and zero-downtime operations. In textile manufacturing, compressed air is not merely a utility; it is a direct production medium. Air-jet looms, pneumatic spinning frames, and automated dyeing systems rely entirely on a continuous, stable, and ultra-clean air supply. Even a microscopic drop of oil or moisture passing through compromised compressor filters can ruin entire batches of high-value fabrics, leading to catastrophic financial losses.
Similarly, in the chemical production sector, the stakes are exceptionally high. Chemical plants operate in highly volatile, corrosive, and demanding environments. Air compressor components such as stainless-steel valves, explosion-proof motors, heavy-duty rotors, and advanced oil separators must withstand extreme temperatures and aggressive chemical vapors. Compressed air is utilized for material agitation, pneumatic conveying of hazardous powders, nitrogen generation, and operating sensitive control valves. The current business reality demands that these parts not only perform flawlessly but also integrate seamlessly into Industry 4.0 paradigms. Plant managers are increasingly investing in high-grade OEM and aftermarket parts that offer extended lifespans, superior wear resistance, and compatibility with predictive maintenance sensors. The cost of a sudden mechanical failure in a chemical oxidation process far exceeds the investment in premium air compressor components.
As global environmental regulations tighten, the focus has shifted heavily towards energy efficiency. Air compressors consume a significant portion of a facility's total electrical power. Upgrading individual parts—such as installing high-efficiency air ends, variable speed drive (VSD) controllers, and low-pressure-drop filtration systems—can yield massive energy savings. This transition is not just an operational upgrade; it is a strategic necessity for textile and chemical enterprises aiming to reduce their carbon footprint and maintain competitive pricing in the global market.

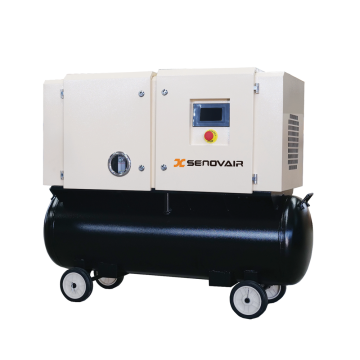
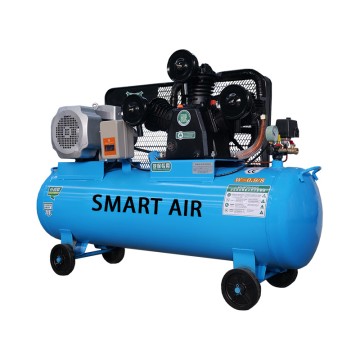
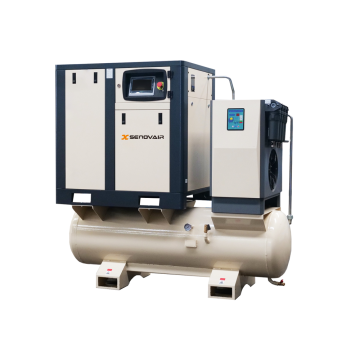
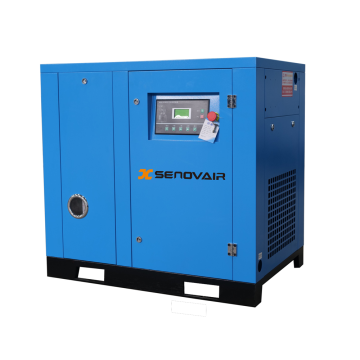
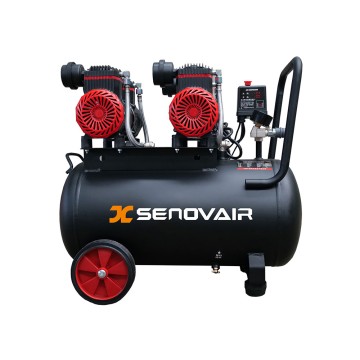
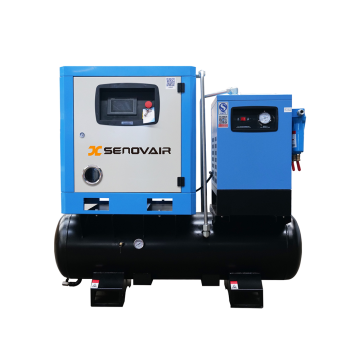
Smart Air Machinery (Linyi) Co., Ltd., established in 2005, is a diversified manufacturing enterprise integrating product research and development, production, and sales. The company employs over two hundred people and primarily manufactures screw air compressors, piston air compressors, air storage tanks, and related machinery tailored for demanding sectors like textile and chemical production.
Established
Employees
Understanding the micro-level applications of air compressor parts for textile and chemical production reveals why standard, off-the-shelf components often fall short. The intersection of mechanical engineering and chemical/textile processing requires bespoke pneumatic solutions. Let us delve into the specific scenarios where high-quality compressor parts make a definitive difference.
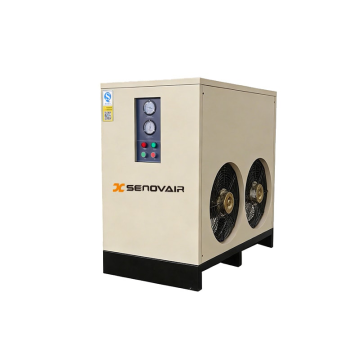
Air-jet looms operate at staggering speeds, using bursts of compressed air to propel the weft yarn across the warp. This requires absolute pressure stability. High-precision intake valves and pressure regulators ensure that the air pulse is perfectly timed and forceful enough to carry the yarn without breaking it. Furthermore, the air must be 100% oil-free and dry. Specialized desiccant dryer parts and coalescing filters are critical here; any moisture will cause the yarn to stick, while oil will stain the fabric permanently.
In chemical synthesis, maintaining uniform temperature and mixture consistency is vital. Compressed air is often bubbled through chemical vats for agitation. The compressor parts involved, especially check valves, piping, and air ends, must be constructed from highly durable, corrosion-resistant alloys. If a standard valve corrodes and fails, chemical backflow into the compressor system can cause catastrophic equipment destruction and severe safety hazards.
The production of PET bottles requires high-pressure compressed air (often up to 40 bar). This necessitates specialized high-pressure booster compressors. The pistons, rings, and cooling heat exchangers in these systems undergo immense thermal and mechanical stress. Utilizing advanced composite materials for piston rings and high-efficiency copper/aluminum fins for coolers ensures continuous 24/7 operation without thermal degradation or pressure drops.
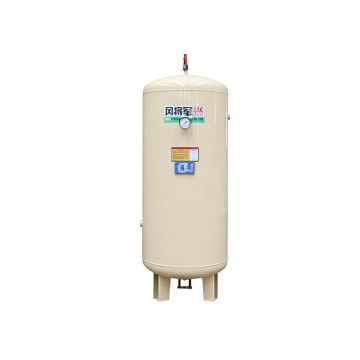
Beyond these direct applications, the role of air receivers (storage tanks) and drain valves cannot be overstated. In textile dyeing, large volumes of air are needed intermittently for fabric transport and dye mixing. High-capacity air tanks stabilize the system pressure, while intelligent electronic zero-loss drain valves automatically expel accumulated condensate without wasting valuable compressed air. Every single part, from the smallest O-ring to the massive twin-screw rotors, forms an interconnected ecosystem of reliability.
Located in Linyi, the logistics capital of China, our company has accumulated rich production experience, strong technical capabilities, a top-notch R&D team, and complete testing equipment through over 20 years of diligent research and continuous innovation.
Our products, known for their aesthetically pleasing design, meticulous material selection, exquisite craftsmanship, and superior quality, are sold worldwide and have received widespread acclaim from customers in the textile and chemical sectors.
Smart Air is committed to building a leading brand in China's air compressor industry. We firmly implement our own brand strategy, adhere to the principle of honest business practices, prioritize customer service, and continuously strengthen our production capabilities.
We firmly believe that "quality creates reputation," "reputation creates brand," and "brand creates market." Currently, we have become a well-known and advanced enterprise in the industry, providing critical components for industrial automation.
As we look towards the future, the evolution of air compressor parts for textile and chemical production is heavily influenced by the megatrends of Industry 4.0, Artificial Intelligence (AI), and sustainable manufacturing. The days of purely mechanical, reactive maintenance are over. Today, compressor parts are becoming "smart." The integration of IoT (Internet of Things) sensors directly into components like bearings, oil filters, and air ends allows for real-time monitoring of vibration, temperature, and pressure differentials.
Predictive Maintenance driven by AI: In a continuous chemical processing plant, unplanned downtime is not an option. AI algorithms now analyze the data streams from smart compressor parts to predict failures before they happen. For instance, a slight increase in the acoustic profile of a screw rotor bearing can trigger an automated alert to replace the part during the next scheduled maintenance window, avoiding a multi-million dollar plant shutdown. This technological leap transforms compressor parts from passive metal objects into active participants in the plant's digital ecosystem.
Advanced Materials and Nanotechnology: The chemical industry's demand for durability is driving innovation in materials science. We are witnessing the rise of advanced ceramic coatings for rotors and Teflon-infused seals that offer unprecedented resistance to chemical attack and high temperatures. In the textile industry, where oil-free air is the holy grail, the development of water-lubricated ceramic rotors and magnetic levitation bearings is eliminating the need for lubricating oil entirely within the compression chamber. These cutting-edge parts ensure absolute air purity while significantly reducing mechanical friction and energy loss.
Energy Recovery Systems: Up to 90% of the electrical energy consumed by an air compressor is converted into heat. Modern compressor parts now include highly efficient heat recovery exchangers. In textile dyeing facilities, the hot water generated from compressor cooling can be directly routed to dye baths, drastically reducing boiler fuel consumption. This holistic approach to system design means that investing in the right compressor parts is no longer just a maintenance cost, but a highly profitable energy-saving strategy that aligns with global carbon neutrality goals.
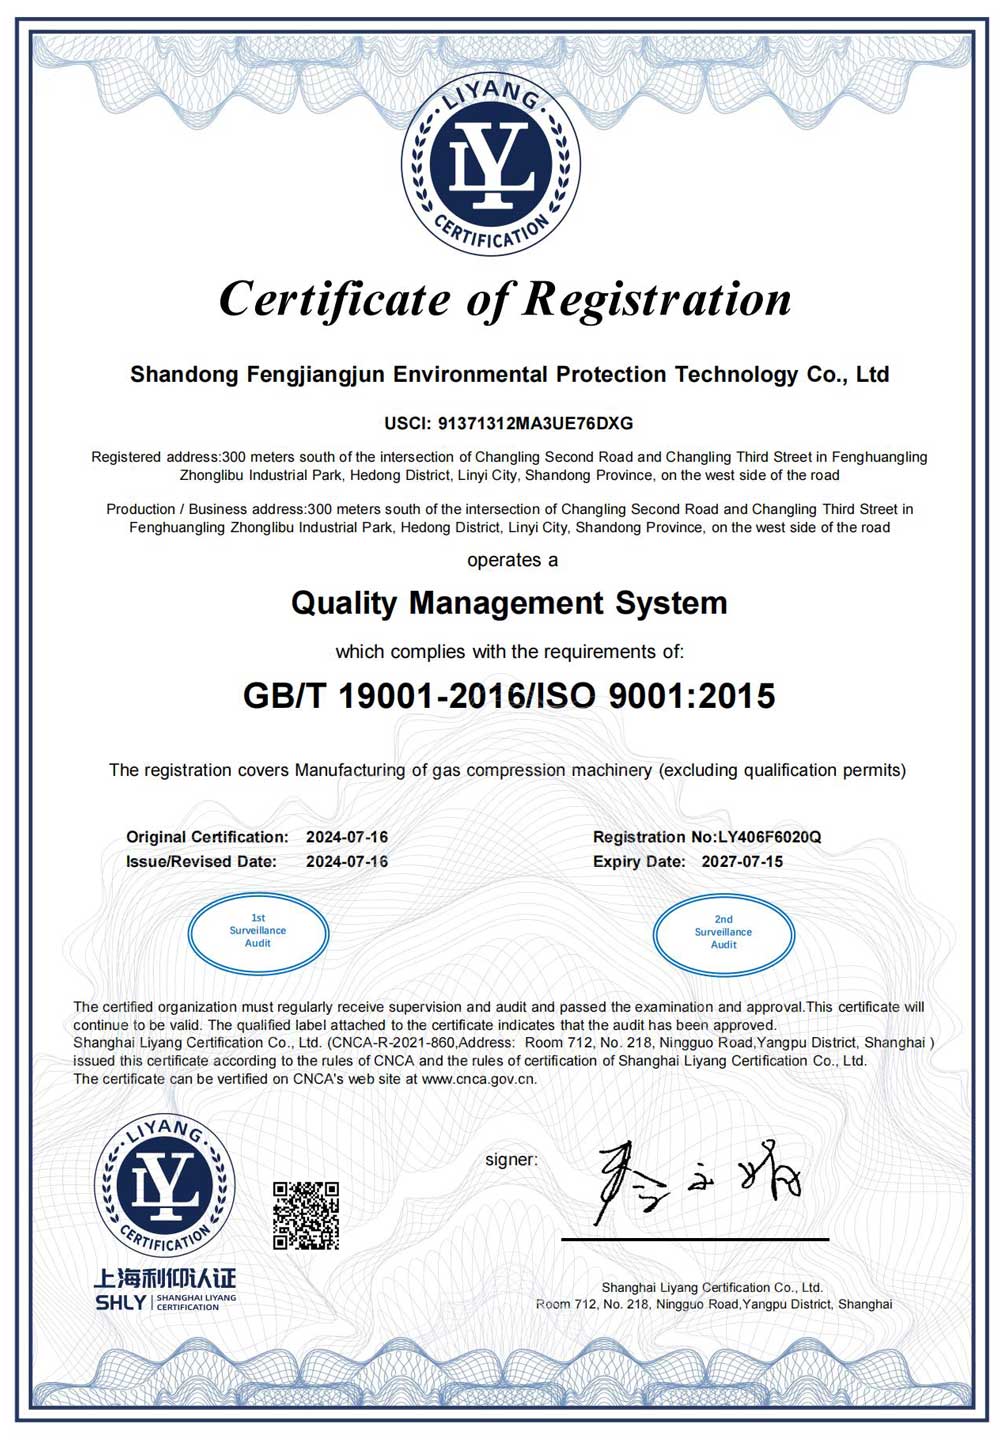
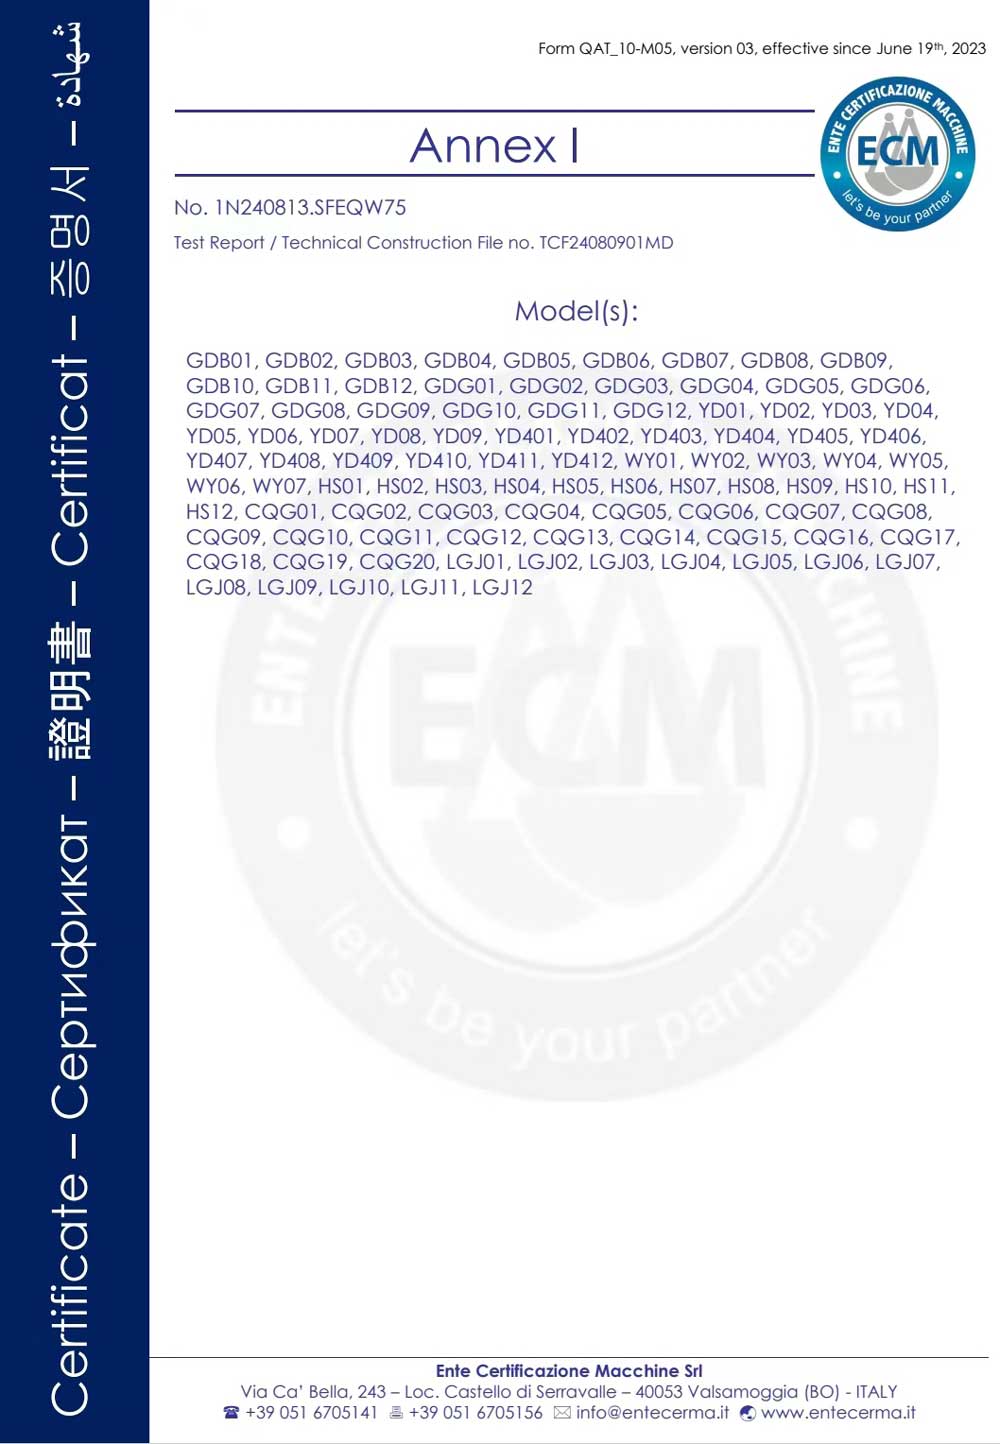
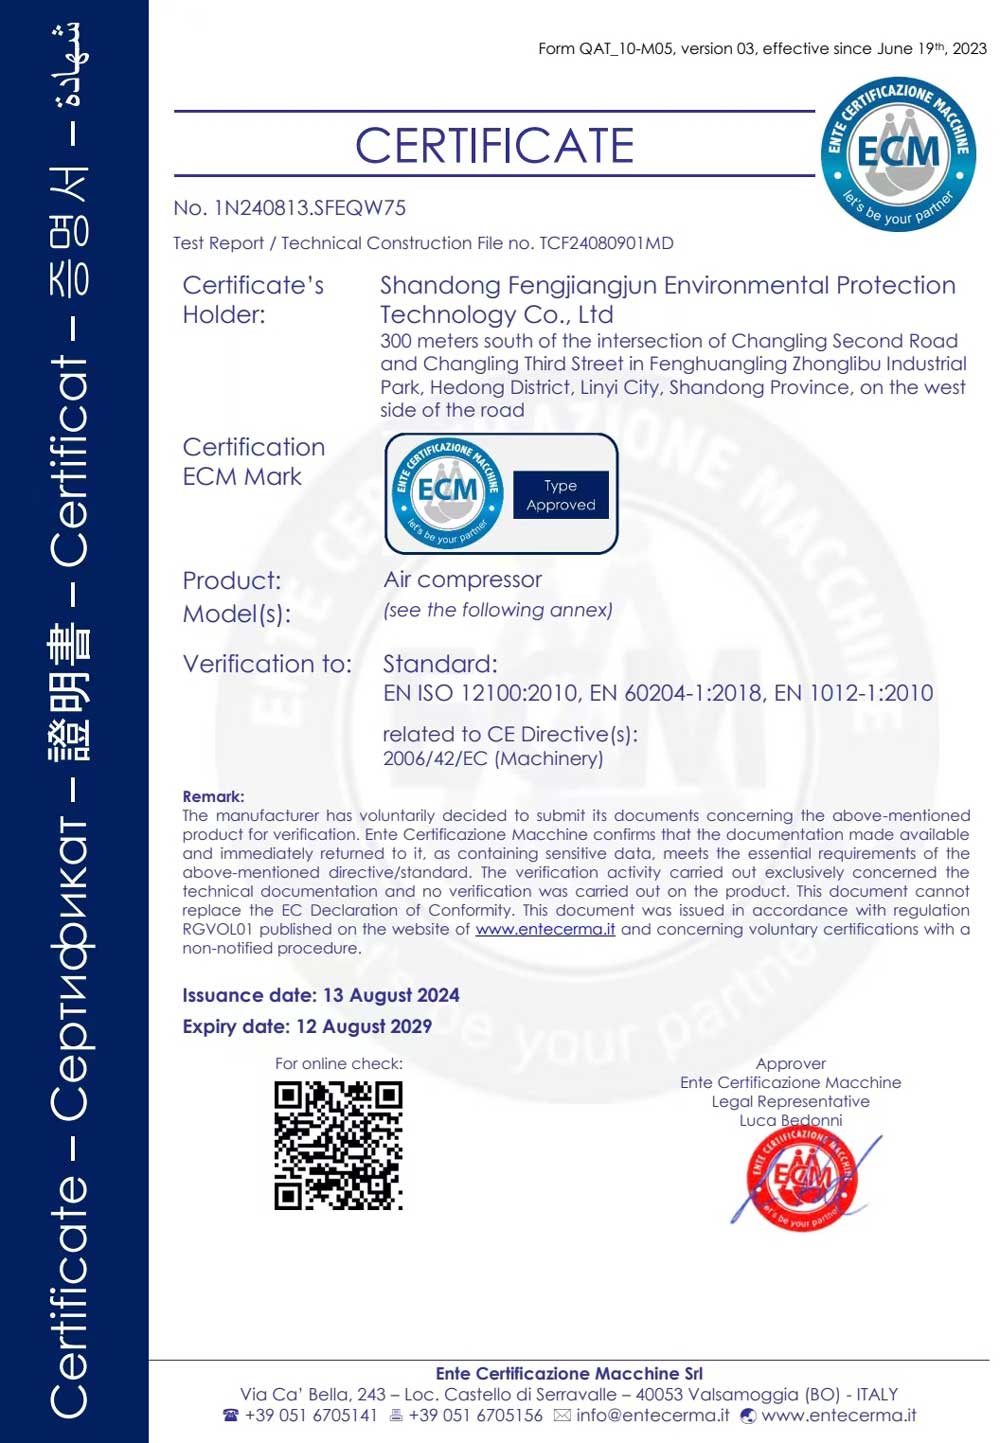
Since its establishment, the company has successively received numerous honors, including "China Famous Brand," "China's Preferred Brand for Green and Environmentally Friendly Products," "Top Ten Foreign Trade Enterprises in the Mall," "High-Tech Enterprise," "3A Credit Enterprise," and "Civilized and Trustworthy Unit."
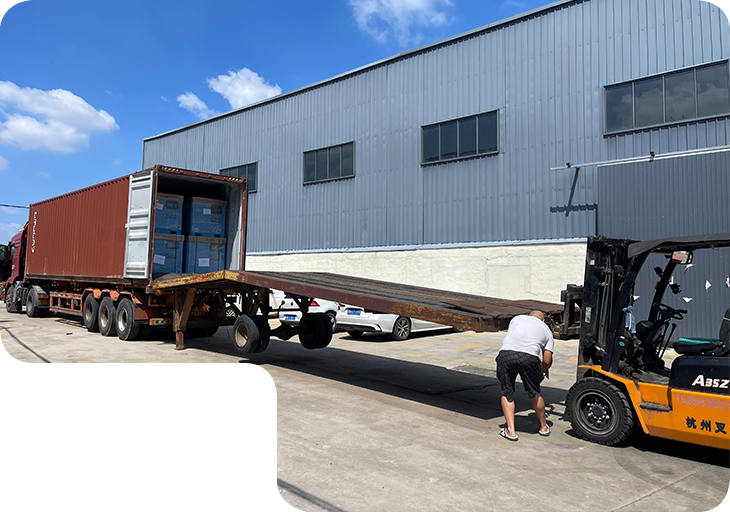
With a proven track record of successful collaborations in over 20 countries, including the USA, Canada, Colombia, Chile, Australia, New Zealand, Russia, Indonesia, Vietnam, Malaysia, India, Sri Lanka, Bangladesh, Pakistan, Dubai, Afghanistan, Israel, Syria, Kosovo, Tunisia, and Angola, we are committed to meeting the diverse needs of our clients. At Smart Air, we pride ourselves on delivering tailored solutions that adhere to the highest standards of quality and performance. Our customers consistently express their satisfaction with our products, praising their reliability and efficiency. Join the growing list of satisfied clients who trust Smart Air for their air compression needs. Experience excellence with us today!
We will always uphold our commitment to warm hospitality and attentive service, and we welcome domestic and international business partners to discuss cooperation.