inquiry
Leave Your Message

Commercial Air Compressors For Textile & Chemical Production

Powering precision, efficiency, and sustainability across global textile mills and chemical manufacturing plants with next-generation compressed air solutions.

🏭 Industrial-Grade  |  🌐 Trusted in 20+ Countries  |  ⚡ IoT-Enabled
$12B+
Global Industrial Air Compressor Market (2024)
38%
Energy Savings via VSD Technology vs. Fixed-Speed
20+
Countries Served by Smart Air Machinery
21
Years of Manufacturing Excellence Since 2005

Why Textile & Chemical Industries Rely on Commercial Air Compressors

From spinning looms to reactor pressurization, compressed air is the invisible backbone of modern manufacturing.

Commercial air compressors are critical utilities in both textile and chemical production environments. In textile manufacturing, compressed air drives pneumatic looms, jet-weaving machines, yarn-tensioning systems, and dyeing equipment — demanding stable pressure, ultra-low moisture content, and uninterrupted supply. In chemical production, compressors handle everything from gas transfer and reactor pressurization to conveying powders and operating control valves, where oil-free air purity and explosion-proof compliance are non-negotiable. As both industries evolve toward smarter, greener operations, the demand for intelligent, energy-efficient, and IoT-connected air compressor solutions is accelerating at an unprecedented pace.

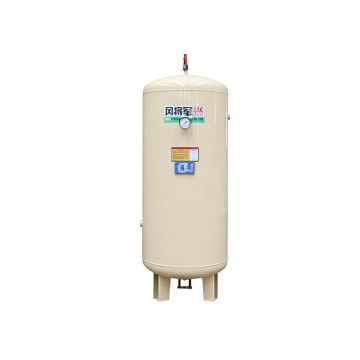
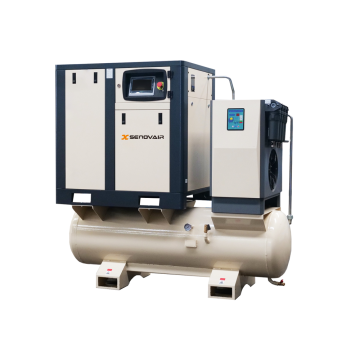
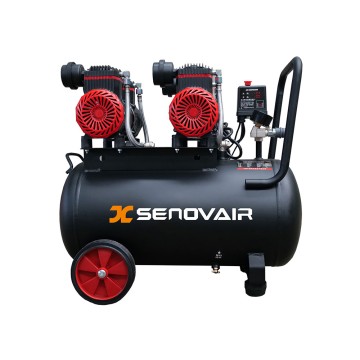
Featured Solutions for Textile & Chemical Production

Deep-Dive Application Scenarios

How commercial air compressors power every critical stage of textile and chemical manufacturing.

🧵

Air-Jet Weaving & Spinning Systems

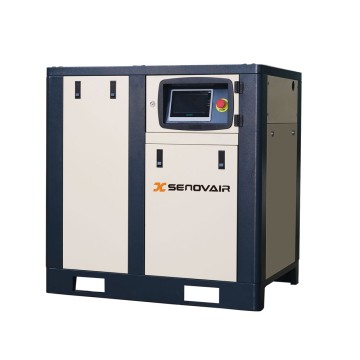
Air-jet looms require a continuous, high-volume air supply at precisely regulated pressure (typically 5–8 bar) to propel yarn across the shed at speeds exceeding 1,000 rpm. Even minor pressure fluctuations cause weaving defects, thread breakage, and costly downtime. PM VSD screw compressors with real-time pressure control are the preferred choice for modern textile mills seeking zero-defect fabric output.

🎨

Dyeing, Finishing & Drying Processes

In textile dyeing and finishing, compressed air is used to atomize dye solutions, agitate liquor in dyeing vessels, and drive pneumatic actuators on finishing frames. Moisture-free, oil-free air is essential here — any contamination can cause uneven coloration or fabric damage. Integrated air dryers and filtration systems ensure ISO 8573 Class 1 purity standards are consistently met.

⚗️

Chemical Reactor Pressurization

Reactors in pharmaceutical and specialty chemical plants require precise pressure management during synthesis, polymerization, and distillation. Screw compressors with variable speed drives maintain consistent inlet pressure, reducing reaction variance and improving yield. Explosion-proof configurations and ATEX-certified models are available for handling flammable or volatile chemical environments.

🔬

Pneumatic Conveying of Chemical Powders

Bulk powder transfer — from pigments and resins to fertilizers and pharmaceutical intermediates — relies on dense-phase or dilute-phase pneumatic conveying systems. High-pressure screw compressors (up to 16 bar) provide the motive force for efficient, contamination-free transport across large chemical complexes, replacing mechanical conveyors that introduce hygiene and maintenance risks.

🌡️

Instrumentation & Process Control Air

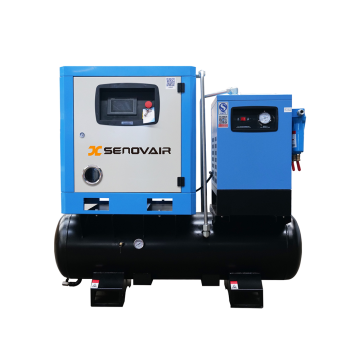
Thousands of pneumatic control valves, positioners, and actuators in a chemical plant depend on instrument air — clean, dry, and oil-free. A single moisture event can freeze a valve or trigger a safety shutdown. Our 4-in-1 integrated systems with built-in refrigerated dryers and coalescing filters guarantee continuous instrument air supply to ISO 8573-1 Class 2 or better.

🏗️

Maintenance, Purging & Plant Utilities

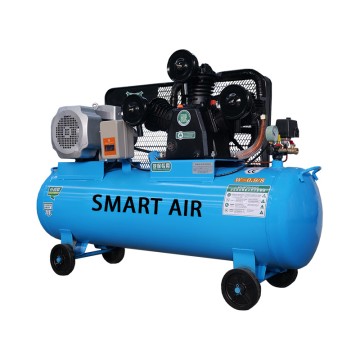
Beyond process applications, mobile piston and portable screw compressors support plant maintenance tasks: pipeline purging, pressure testing, pneumatic tool operation, and tank blanketing with inert gases. Their wheel-mounted mobility allows rapid deployment across sprawling chemical plant sites or multi-building textile campuses without fixed installation costs.

💡

Key Insight: Energy Costs Account for 70–80% of Total Air Compressor Lifecycle Cost

Selecting a PM VSD (Permanent Magnet Variable Speed Drive) screw compressor over a fixed-speed model can reduce energy consumption by up to 38%, delivering ROI within 18–24 months in continuous-operation textile and chemical facilities. Smart Air's IoT-enabled monitoring system further identifies inefficiencies in real time.

Industry Trends Shaping the Future of Compressed Air in Manufacturing

The commercial air compressor landscape is undergoing rapid transformation driven by digitalization, sustainability mandates, and evolving production demands.

🤖

IoT & Industry 4.0 Integration

Modern compressors are no longer standalone machines — they are connected nodes in smart factory ecosystems. IoT-enabled compressors transmit real-time data on pressure, temperature, energy consumption, and maintenance alerts to centralized dashboards. In chemical plants, this enables predictive maintenance, reducing unplanned downtime by up to 45% and extending equipment lifespan significantly.

🌱

Green Manufacturing & Carbon Neutrality Goals

With the textile industry responsible for approximately 10% of global carbon emissions, and chemical manufacturing under increasing regulatory pressure, energy-efficient compressors are central to decarbonization strategies. Heat recovery systems that capture up to 96% of compression heat for process heating are becoming standard in new textile and chemical plant designs across Europe and Asia.

⚡

Variable Speed Drive (VSD) Adoption Surge

The global VSD compressor market is projected to grow at a CAGR of over 6% through 2030, driven by energy cost pressures and stricter efficiency standards. Textile mills with highly variable air demand — common during shift changes or seasonal production peaks — benefit enormously from VSD technology that automatically matches output to real-time demand without energy waste.

🛡️

Oil-Free Technology for Pharmaceutical & Specialty Chemicals

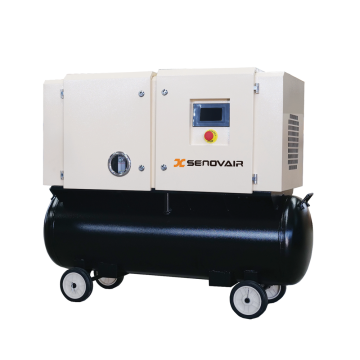
Regulatory requirements in pharmaceutical chemical manufacturing (GMP compliance, FDA standards) are accelerating the shift to certified oil-free compressors. Class 0 oil-free models eliminate any risk of product contamination, protecting both brand integrity and patient safety. Smart Air's oil-free portable range addresses this growing segment with reliable, compact solutions.

🔗

Modular & Scalable Compressed Air Systems

As textile and chemical companies expand capacity incrementally, modular compressor systems that allow easy capacity addition without full system redesign are gaining traction. Our 2-in-1 and 4-in-1 integrated compressor platforms exemplify this trend, combining compression, drying, filtering, and storage in a single footprint-optimized unit that scales with production growth.

🌏

Emerging Market Expansion in Asia & Africa

Rapid industrialization in Bangladesh, Vietnam, India, Pakistan, and sub-Saharan Africa is creating massive demand for affordable, reliable commercial air compressors in textile manufacturing. Smart Air's global distribution network and multilingual technical support position us as the preferred partner for greenfield textile and chemical plant projects in these high-growth markets.

Smart Air Machinery - 21 Years of Experience in Commercial Air Compressors
21 Years
Of Experience

Company Profile — Smart Air Machinery (Linyi) Co., Ltd.

Smart Air Machinery (Linyi) Co., Ltd., established in 2005, is a diversified manufacturing enterprise integrating product research and development, production, and sales. The company employs over two hundred people and primarily manufactures screw air compressors, piston air compressors, air storage tanks, and related machinery.

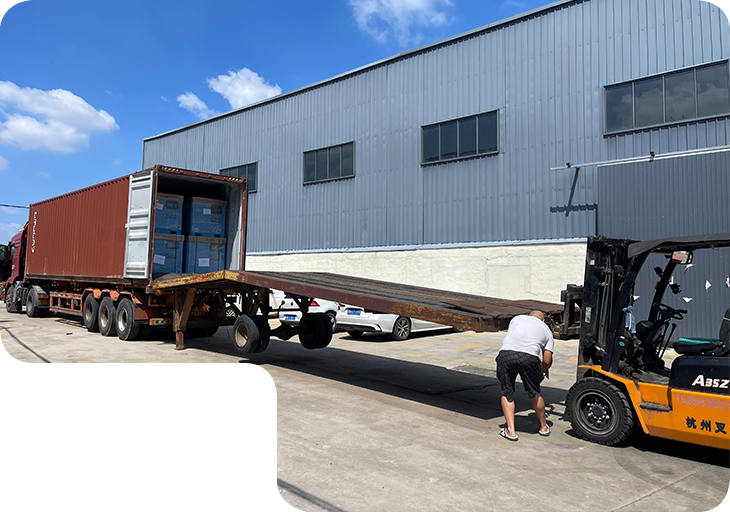
Located in Linyi — the logistics capital of China — we have built a reputation for delivering world-class compressed air solutions to textile mills, chemical plants, and industrial facilities across more than 20 countries. Our state-of-the-art manufacturing facility combines advanced CNC machining, rigorous quality inspection, and continuous R&D investment to ensure every compressor we ship meets the highest international standards.

2005
Established
200+
Employees
20+
Countries Served

Why Choose Smart Air for Your Textile & Chemical Compressed Air Needs

🏛️

Company Heritage & Technical Depth

Located in Linyi, the logistics capital of China, our company has accumulated rich production experience, strong technical capabilities, a top-notch R&D team, and complete testing equipment through over 20 years of diligent research and continuous innovation. Our engineers specialize in compressed air system design for both textile and chemical production environments.

⭐

Product Advantages & Superior Quality

Our products, known for their aesthetically pleasing design, meticulous material selection, exquisite craftsmanship, and superior quality, are sold worldwide and have received widespread acclaim from customers. Every unit undergoes full-load factory testing before shipment, ensuring reliable performance from day one in your production facility.

🚀

Brand Strategy & Global Commitment

Smart Air is committed to building a leading brand in China's air compressor industry. We firmly implement our own brand strategy, adhere to the principle of honest business practices, prioritize customer service, continuously strengthen our production capabilities, and constantly enhance our brand influence in the textile and chemical sectors globally.

🏆

Quality Philosophy & Proven Track Record

We firmly believe that "quality creates reputation," "reputation creates brand," and "brand creates market." Currently, we have become a well-known and advanced enterprise in the industry, recognized with honors including "China Famous Brand," "High-Tech Enterprise," and "3A Credit Enterprise" — assurances that matter when selecting a long-term compressed air partner.

Our Certifications & Industry Recognition

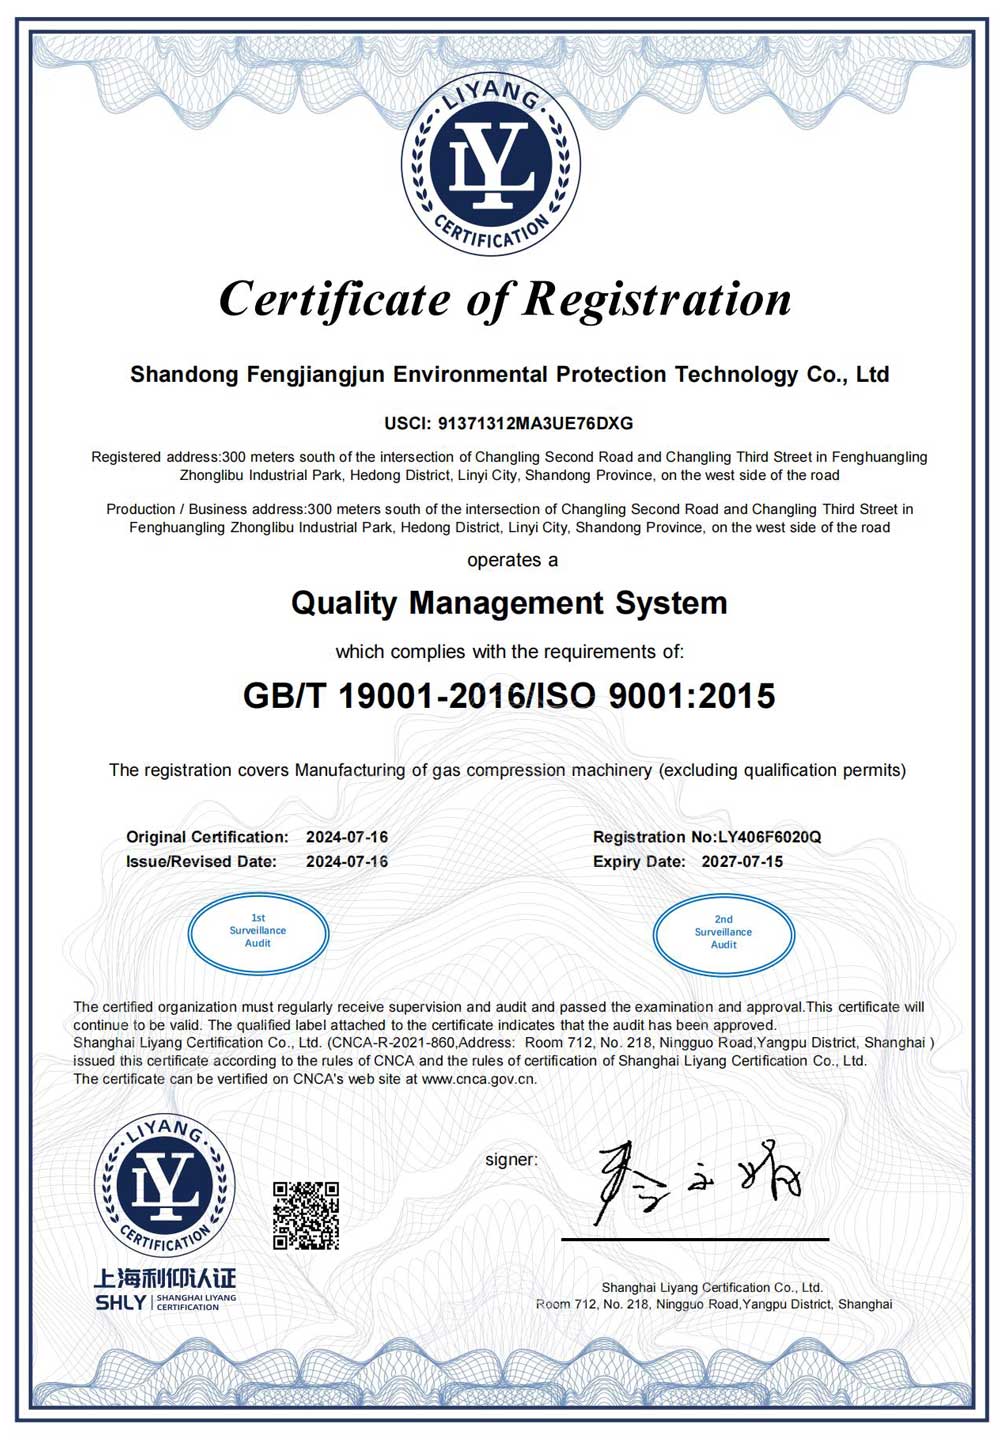
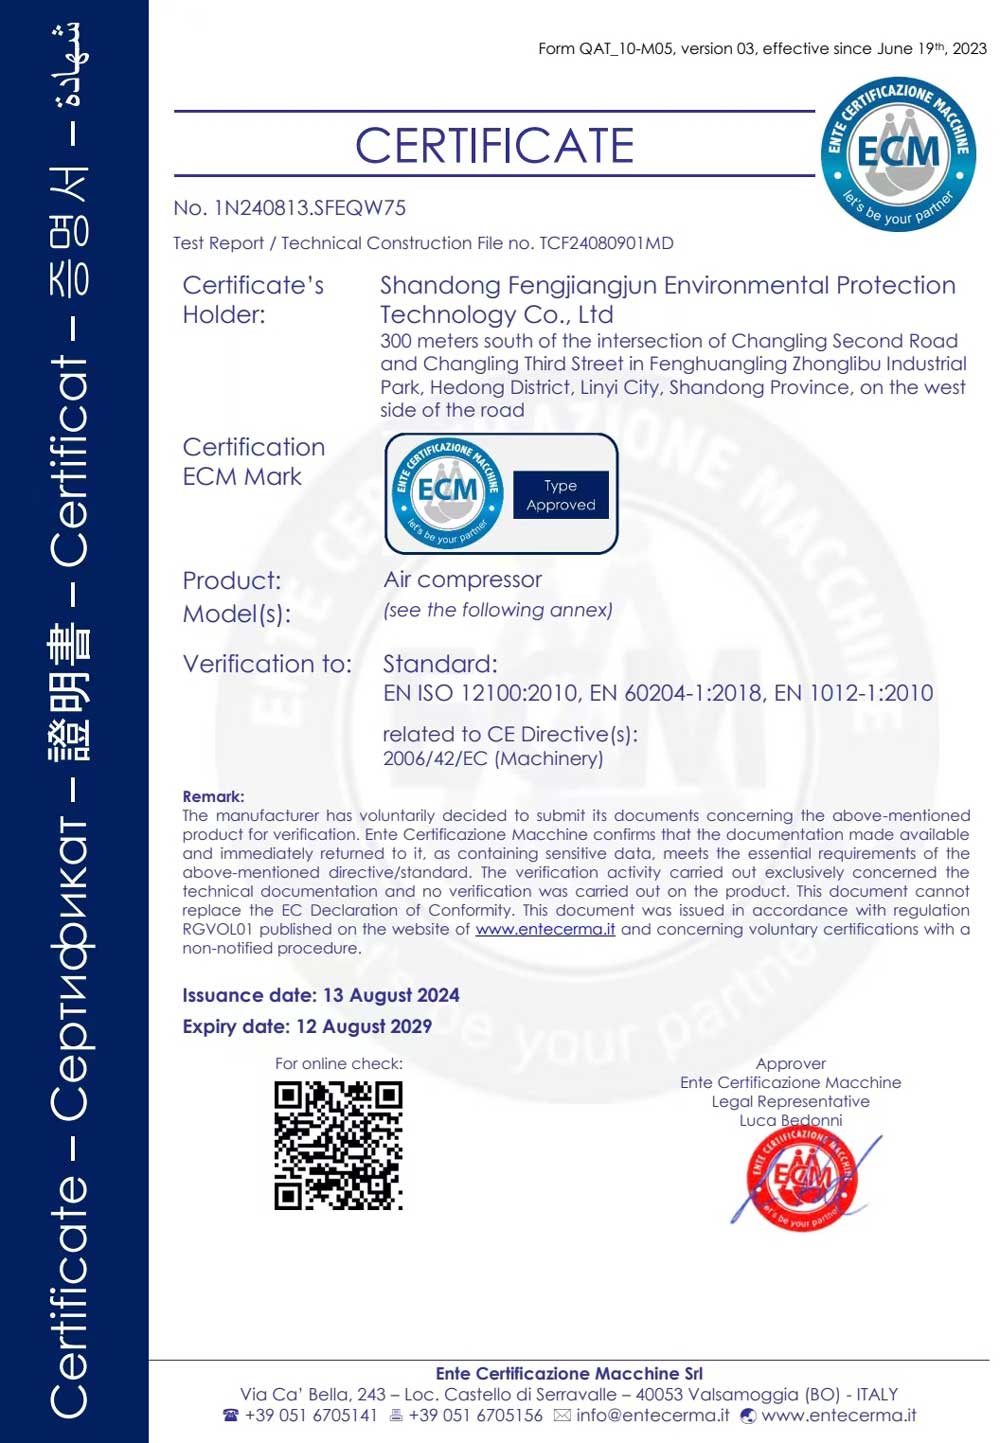
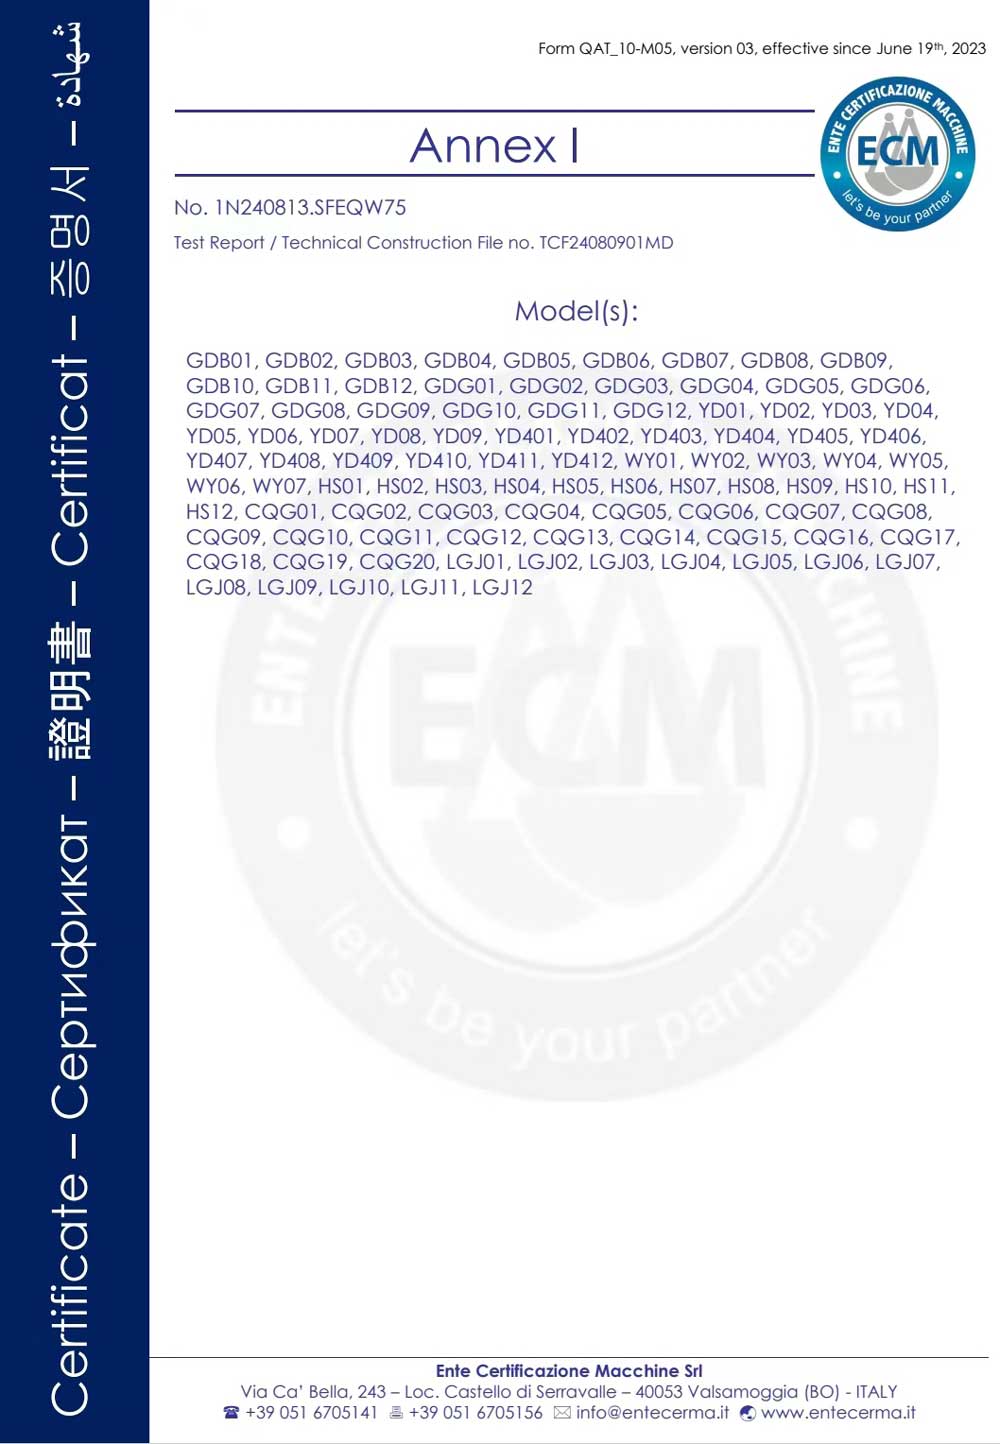
Since its establishment, the company has successively received numerous honors, including "China Famous Brand," "China's Preferred Brand for Green and Environmentally Friendly Products," "Top Ten Foreign Trade Enterprises in the Mall," "High-Tech Enterprise," "3A Credit Enterprise," and "Civilized and Trustworthy Unit."

With a proven track record of successful collaborations in over 20 countries, including the USA, Canada, Colombia, Chile, Australia, New Zealand, Russia, Indonesia, Vietnam, Malaysia, India, Sri Lanka, Bangladesh, Pakistan, Dubai, Afghanistan, Israel, Syria, Kosovo, Tunisia, and Angola, we are committed to meeting the diverse needs of our clients. At Smart Air, we pride ourselves on delivering tailored solutions that adhere to the highest standards of quality and performance. Our customers consistently express their satisfaction with our products, praising their reliability and efficiency. Join the growing list of satisfied clients who trust Smart Air for their air compression needs. Experience excellence with us today!

We will always uphold our commitment to warm hospitality and attentive service, and we welcome domestic and international business partners to discuss cooperation.

Smart Air Machinery Certificate 1Smart Air Machinery Certificate 3Smart Air Machinery Certificate 2

Complete Product Range for Textile & Chemical Industry Applications

Explore our full lineup of commercial air compressors and after-treatment solutions engineered for demanding industrial environments.